Two Runs a Day Is a Habit, Not a Strategy: Stocking a Consumables Bench
Every mason reading this has done it. You're two cuts from finishing a sill, the 115mm disc is down to a nub, and someone's driving to the merchant. Then it happens again at three o'clock because nobody checked the fixings.
Individually, each run is twenty minutes. Collectively, it's a line item nobody has ever costed.
What the Second Run Actually Costs
Do the arithmetic on your own shop, not mine, but here's the shape of it. A merchant trip from a typical small unit:
| Element | Typical |
|---|---|
| Travel, each way | 15–20 min |
| Parking and queue | 10 min |
| Picking and paying | 10–15 min |
| Total lost time | 50–75 min |
Two people on the clock at a modest £45/hour charge-out equivalent means that trip costs £75–£110 in labour before you buy anything. Add fuel at £6–£8. Now look at the frequency: if it's twice a week, that's roughly £8,000–£12,000 a year of shop time spent buying £40 of discs.
And the real damage isn't the labour. It's the knock-on. A run at 10:30 means the bench sits idle, the second fix slips to the afternoon, and someone ends up working late to hit a deadline that was never in doubt on Monday morning.
There's also the invisible tax: buying in panic. When you're standing in the branch with a job waiting, you buy whatever's on the shelf at whatever price. That's how a shop ends up paying premium rates for a disc it could have bought in a box of ten.
The Consumables That Actually Matter
You can't stock everything. You can stock the twenty or so lines that stop a job dead.
Cutting — 115mm and 230mm diamond discs in the grits you actually use, a spare 300/350mm blade for the bench saw, and a core drill bit for the sizes you quote regularly.
Finishing — resin-bond polishing pads in the full sequence, flap discs, grinding cups, and the backing pad that always fails at the worst time.
Fixing — the three or four anchor and screw types that appear on 80% of your work, plus the washers nobody remembers.
Sealing and bonding — one silicone in the colours you use, one hybrid, one epoxy, one polyester resin.
PPE — respirator filters (these have a life, so watch it), gloves, eye protection, ear defenders.
The small stuff — chalk, pencils, masking tape, cable ties, PTFE tape, marker pens. Cheap individually, infuriating to run out of.
Anything beyond that list is a special purchase. That's fine. Special purchases get planned, not improvised.
Setting Min, Max and Reorder Points
Keep it simple enough that it survives a busy week.
Minimum level = typical weekly usage × supplier lead time in weeks, plus a buffer of about a third.
If you get through four 115mm discs a week and your supplier is three working days away, you need roughly 2 discs of cover plus buffer — call it 3. Round up to a sensible pack size.
Maximum level = minimum + one sensible reorder quantity. Not two pallets, just enough that you're not ordering singles.
Reorder point = the minimum. When you hit it, you order. Not when you're down to the last one.
Write these three numbers on the shelf edge. Not in a spreadsheet that gets opened quarterly — on the shelf, at eye level, in marker pen.
Lead Times: Buy the Delay, Not the Discount
Not all consumables are equal. Rough UK lead times to plan around:
- Standard discs, abrasives, fixings, PPE — next day to three days from most UK trade suppliers.
- Bench saw blades in non-standard sizes — five to seven days, often longer if it's a special bore.
- Colour-matched sealants and specialist resins — five to ten days.
- Anything imported — assume two weeks and be pleased when it's quicker.
The trap is chasing a 10% discount on a five-day lead time item. On a four-week job that's fine. On a two-day job it's a disaster. Match the buying method to the lead time, not to the discount.
A Stock Card System That Survives Real Life
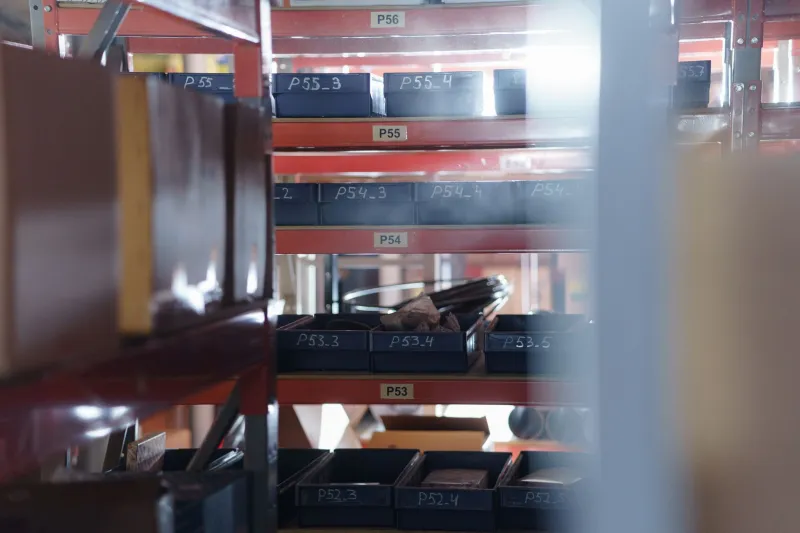
You don't need software. You need an A6 card per line, kept in a little box on the bench, and a rule that whoever takes the last one writes on the card.
Each card carries:
- Item and size
- Supplier and account reference
- Lead time in working days
- Min / max / reorder quantity
- A running tally of the last four order dates
That last one is the useful bit. After two months you can see actual usage instead of guessing, and you'll spot the lines where the min is set way too low.
Label the shelf to match the card. Colour-code by supplier so whoever does the order can walk the shelves in one pass rather than three. It sounds fussy. It takes an hour to set up and it saves a morning a week.
The Two-Bin Trick
For the high-turnover lines — discs, pads, gloves, screws — split the stock into two bins. When the front bin empties, it goes on the order hook, you start on the back bin, and nobody has to remember anything. Reorder happens automatically because the empty bin is physically in your way.
It's a factory idea, and it works in a two-man stone shop precisely because it removes the need for anyone's memory.
Shelf Life, Frost and the Stuff You Shouldn't Hoard
Stock control isn't only about having enough. It's about not having too much of the wrong thing.
- Resins, silicones and adhesives have shelf lives — typically 9–18 months. Buy to usage, not to discount. Write the delivery date on the tube.
- Frost kills sealants. If they live in the van over winter, they're degrading. Store them in the shop, frost-free, and load only what the day needs.
- Diamond doesn't expire. Discs and blades can sit indefinitely, so a box of ten is genuinely cheaper than ten singles — as long as you're not tying up cash you need for something else.
- Respirator filters have a service life once opened. Date them.
Review It Once a Quarter
Twenty minutes, four times a year. Look at the stock cards, bin anything that hasn't moved in six months, adjust the mins that keep triggering, and check whether a supplier's lead time has drifted.
The goal isn't a beautiful stockroom. It's finishing the day without a van leaving the yard at half ten, and buying your consumables at trade prices, in planned quantities, on a weekday when nobody's waiting for you.